A Custom Charger Plate Mold is normally a one-time tooling investment used to manufacture an exclusive charger plate shape or structure. For B2B projects, tooling may range from a few thousand dollars to much more depending on plate size, mold steel, surface detail, cavity design and expected mold life. Tool development commonly takes several weeks, while production MOQ is usually determined separately by material, finishing, color and packaging requirements.
That distinction matters.
Many importers ask three questions at the same time:
- How much is the mold?
- What is the MOQ?
- How long will the project take?
They look like simple questions, but they involve different parts of the manufacturing process.
A buyer may pay for only one mold, yet order thousands of charger plates from it. Likewise, a factory may technically be able to inject 500 pieces, but a special electroplated finish or custom gift box may require a higher commercial MOQ.
That’s why an accurate quotation should separate tooling cost, product cost, decoration cost, packaging cost and development time.
For distributors, event-supply brands, hospitality wholesalers and private-label tableware companies, understanding these items before paying a tooling deposit can prevent expensive redesigns later.
Custom Charger Plate Mold: Cost, MOQ and Lead Time
For budgeting purposes, buyers should think of a charger plate program as four connected investments rather than one price:
| Project Element | What You Are Paying For | Main Cost Driver |
|---|---|---|
| Mold / tooling | Equipment used to form the plate | Size, steel, structure, complexity |
| Molded plate | Plastic base product | Resin weight, cycle time, quantity |
| Decoration | Paint, plating, printing or texture | Finish complexity and reject rate |
| Packaging | Inner pack, carton, retail packaging | Packing style and order quantity |
Public supplier listings show why tooling prices should never be treated as one fixed industry number. Current listings for plastic plate and tableware molds span roughly US$1,000 to US$10,000 and beyond, with some more complex molds quoted substantially higher. These marketplace figures are useful only as reference points because the technical specification behind each mold varies.
For a charger plate, diameter also matters. A typical decorative charger is much larger than a small molded component. More steel, a larger mold base and a suitable injection machine may therefore be required.
A practical RFQ should define at least:
- Outside diameter
- Overall height
- Rim width
- Plate thickness
- Bottom structure
- Surface texture
- Required material
- Decoration process
- Annual volume
- Expected mold life
Without these details, two quotations that look similar may actually describe very different tools.
Why Custom Charger Plate Tooling Is Different From Standard Products
If you choose a charger plate from a manufacturer’s existing collection, there may be no new mold charge at all.
The factory already owns the tooling. You simply select the existing shape and customize elements such as color, surface coating, logo, label or packaging.
Creating a completely new shape changes the project.
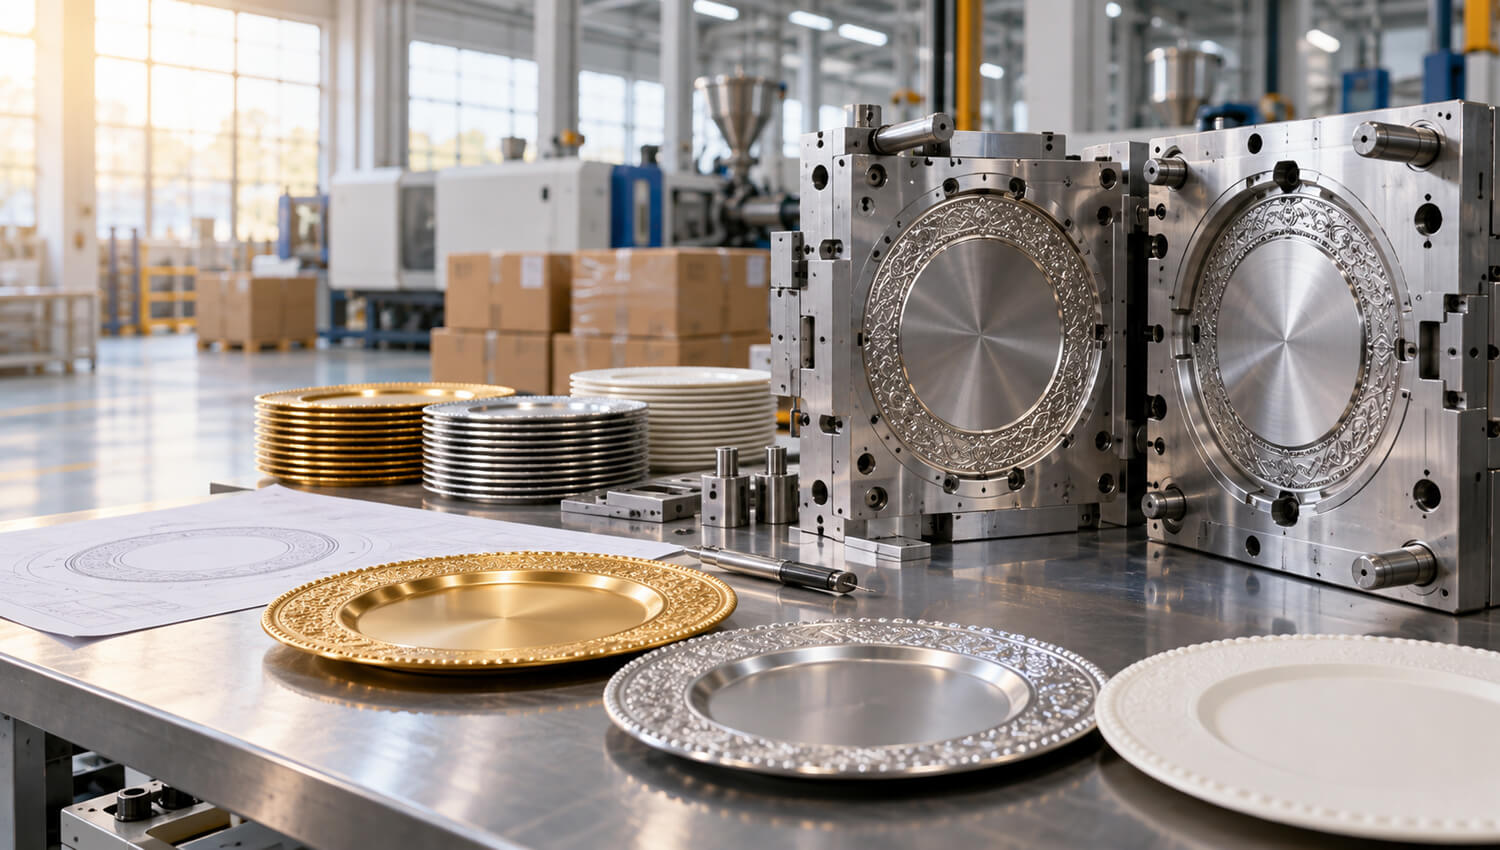
Imagine that you want a 13-inch charger plate with a wide irregular rim, embossed geometric pattern and special raised edge. The manufacturer cannot create that geometry by changing only the paint color. A new cavity and core must be engineered.
This development process may involve:
- 2D dimensional drawings
- 3D CAD modeling
- Design-for-manufacturing review
- Shrinkage allowance
- Gate-position planning
- Cooling design
- Ejection design
- CNC machining
- EDM work where necessary
- Polishing or texturing
- Mold assembly
- Mold trials
- Dimensional corrections
The practical difference for buyers is important.
Existing mold customization is usually suited to fast private-label programs.
New tooling is better when you need genuine product differentiation.
For example, a distributor may want exclusive rim architecture so competitors cannot source an identical plate from another supplier. A hotel-supply brand may need a charger that matches an existing dinnerware collection. A retailer may want an identifiable pattern that becomes part of its brand language.
In these cases, tooling should be treated as an asset used to create repeatable production, not simply as an extra setup fee.
How Much Does a Custom Charger Plate Mold Cost?
There is no reliable universal mold price.
Even large injection-molding companies explain that tooling cost depends strongly on manufacturing time and part complexity. Features such as undercuts, difficult geometry and advanced finishes generally increase tooling cost because they require additional machining and mold mechanisms.
For early sourcing discussions, the following table can be used as a planning framework rather than a guaranteed quotation:
| Project Type | Relative Tooling Cost | Typical Characteristics |
|---|---|---|
| Simple round plate | $ | Basic rim, simple release, limited detail |
| Decorative rim design | $$ | Embossing, texture or more CNC work |
| Premium high-gloss plate | $$–$$$ | Better polishing and tighter cosmetic control |
| Deep or complex geometry | $$$ | More difficult filling and ejection |
| Undercut / special mechanism | $$$$ | Slides, inserts or additional mold actions |
| Multi-cavity tooling | Higher initial investment | Greater production capacity |
Public China-based plastic plate mold listings commonly advertise molds in ranges such as about US$2,000–US$8,000, while other plate and container tools appear above this range. Those listings illustrate market variation rather than establishing a charger-plate price standard.
International rapid-tooling benchmarks show the same pattern. For example, Protolabs states that aluminum tooling can start around US$1,500, while long-life steel tooling requires a much higher investment in some applications.
Therefore, asking only “How much is one mold?” isn’t enough.
Ask instead:
“What tooling specification is included in this price?”
That question gives you something you can actually compare.
What Actually Changes the Tooling Price?
Several engineering details can make two charger plates of the same diameter cost very different amounts to tool.
Plate Diameter and Mold Size
A larger product normally needs a larger mold base. Larger tooling requires more steel and longer machining time.
It may also require a larger injection molding machine.
Rim Geometry
A smooth circular rim is generally easier than a highly ornamental rim with deep relief.
Detailed leaf patterns, bead designs, faceted surfaces and irregular edges require more machining.
Surface Finish
A texture built into the mold is different from a texture created later through paint or coating.
High-gloss surfaces can require careful polishing. Protolabs notes that cosmetic finish requirements influence manufacturing complexity and rapid-tool eligibility.
Undercuts
An undercut prevents the product from releasing directly from the mold.
If the design requires sliders, lifters, inserts or other mechanisms, tooling becomes more complicated.
Steel Specification
A short commercial program and a long-term high-volume program may not need the same tooling material.
Harder mold steels can improve wear resistance and tool longevity, but machining and heat treatment may increase cost.
Runner and Gate Design
The manufacturer must deliver resin into a wide circular product without creating unacceptable flow marks, sink marks, warpage or cosmetic defects.
Gate location is especially important for visible decorative products.
In other words, your mold quotation isn’t simply paying for a metal object. You’re paying for a production system that has to repeatedly create the same geometry.
Custom Charger Plate Mold MOQ Explained
One of the biggest misunderstandings in B2B sourcing is assuming that a tooling MOQ and a production MOQ are the same thing.
They aren’t.
The mold quantity is normally simple:
You generally need one set of tooling to begin production.
Public mold listings frequently show an MOQ of one mold or one set.
The finished charger plate MOQ is different.
Several minimum quantities may exist inside one project.
| MOQ Type | Why It Exists |
|---|---|
| Injection MOQ | Machine setup and production efficiency |
| Resin color MOQ | Material preparation and color matching |
| Painting MOQ | Spray-line setup |
| Electroplating MOQ | Batch processing requirements |
| Printing MOQ | Screen, transfer or printing setup |
| Packaging MOQ | Printed box or carton supplier minimum |
| Order MOQ | Commercial requirement set by supplier |
This explains a common sourcing situation.
A factory may say:
Injection molding can start at 1,000 pieces.
But after you request five Pantone colors with 200 pieces per color, production becomes less efficient.
Or the factory may agree to manufacture 1,000 plates, while the printed retail box supplier requires 3,000 boxes.
For this reason, buyers should ask:
“What is the MOQ for the base product, each color, each finish and custom packaging?”
That question is much more useful than asking for only one general MOQ.
How Mold Design Affects Unit Cost at Different Order Volumes
Tooling cost should not be evaluated separately from expected production volume.
Suppose Project A uses a lower-cost mold but runs slowly.
Project B uses more expensive tooling but shortens cycle time and produces more stable parts.
If your total order is only 3,000 pieces, Project A may be reasonable.
If your annual demand reaches 200,000 pieces, the higher-quality tooling may produce a lower total cost over the program’s life.
The basic calculation is:
Tooling Cost per Plate = Total Mold Investment ÷ Total Units Produced
For example:
| Tooling Investment | Lifetime Production | Tooling Cost Allocated per Plate |
|---|---|---|
| $4,000 | 5,000 pcs | $0.80 |
| $4,000 | 20,000 pcs | $0.20 |
| $4,000 | 100,000 pcs | $0.04 |
| $4,000 | 200,000 pcs | $0.02 |
This is why experienced buyers often focus more on total landed cost and projected volume than mold price alone.
Multi-cavity tooling creates another trade-off.
More cavities can improve production capacity because several products are molded during one machine cycle. However, a large charger plate consumes significant mold area. The injection machine, mold dimensions and shot capacity all become important.
For many large decorative plates, a single-cavity solution may therefore be perfectly reasonable.
Protolabs similarly notes that cavity count and tooling strategy can reduce piece-part pricing at larger volumes, while increasing initial tooling investment.
Custom Charger Plate Mold Lead Time From Drawing to Mass Production
Buyers often hear phrases such as “30-day tooling” and assume finished products will ship 30 days after the deposit.
That isn’t always what the quotation means.
Tooling lead time can describe only the period required to produce the mold.
Your complete project timeline should include several additional steps.
Typical Development Flow
Drawing confirmation → DFM review → mold design → machining → assembly → first mold trial → sample inspection → modification → approval → mass production → finishing → packing
For standard injection-molded parts, rapid tooling companies demonstrate that simple tools can sometimes be produced extremely quickly. Protolabs lists prototype tooling lead times as fast as around seven days in qualifying projects, while Xometry states that some prototype injection molds can be produced in several weeks or less.
However, a decorative charger plate project should not automatically be planned around those rapid-service benchmarks.
A safer commercial schedule may include:
| Stage | Planning Allowance |
|---|---|
| Design confirmation | 2–7 days |
| DFM and mold design | 3–7 days |
| Mold manufacturing | 20–40+ days |
| First trial | 1–3 days |
| Sample review | 3–7 days |
| Modification if needed | 3–14+ days |
| Production | Depends on quantity |
| Surface decoration | Depends on process |
| Packaging | Depends on specification |
The important word is approval.
A mold may technically be finished, yet mass production should not start until the buyer approves the production sample.
A Typical Custom Mold Development Process
A strong mold project begins before steel is cut.
RFQ and Requirement Review
The buyer sends the factory:
- Product dimensions
- Reference photos
- 2D or 3D files when available
- Required material
- Estimated annual volume
- Surface requirements
- Logo requirements
- Packaging expectations
- Destination market
If you only have a physical sample, the manufacturer may reverse-engineer the basic dimensions.
3D Design and DFM
The engineering team converts the concept into manufacturable geometry.
At this stage, buyers should review the shape carefully.
Moving a decorative line in CAD may take minutes.
Moving it after the mold has been machined may require welding, re-machining or even a new cavity.
Tooling Approval
Before tooling starts, confirm:
- Final drawing revision
- Overall dimensions
- Mold material
- Cavity number
- Expected mold life
- Surface specification
- Logo position
- Ownership terms
T0 or T1 Trial
The first mold trial is an engineering checkpoint.
It may reveal:
- Warpage
- Short shots
- Flow marks
- Sink marks
- Ejection marks
- Dimensional differences
- Uneven rim appearance
Corrections at this stage are normal in custom manufacturing.
The goal isn’t to pretend that the first sample is always perfect. The goal is to identify issues before thousands of units are produced.
Golden Sample Approval
Once approved, keep one final signed sample or clearly identified production standard.
That sample becomes the reference for future production and quality inspections.
Material, Finish and Decoration Choices Buyers Should Confirm Early
The mold creates the underlying plate shape.
It does not automatically determine the final visual effect.
A single molded base can potentially support several decorative programs.
For example, a buyer may use the same base geometry for:
- Glossy solid colors
- Matte colors
- Metallic finishes
- Antique effects
- Printed patterns
- Marble effects
- Wood-look transfer patterns
- Seasonal designs
This is an important commercial benefit.
Instead of opening a new mold for every collection, you may develop one core shape and multiple finishes.
However, decoration must be considered during product design.
A narrow embossed rim may look attractive in CAD but prove difficult to coat consistently.
A very deep texture may collect paint.
A high-gloss surface may make cosmetic imperfections easier to see.
A transparent or highly reflective product may require better polishing of the mold surface.
Material choice also affects processing.
Rapid injection molding references point out that different plastics behave differently during molding and that resin choice can influence both moldability and production cost.
Before paying for tooling, ask the manufacturer to confirm the intended resin and decoration system together.
For decorative charger plates, also clearly define whether the item is intended only as a decorative underplate or for direct food contact. Regulatory requirements and material documentation may differ by intended use and destination market.
How to Reduce Mold Cost Without Weakening the Product
Reducing cost doesn’t always mean selecting cheaper steel.
Often, the better approach is improving the product design before machining begins.
Remove Unnecessary Undercuts
Undercuts may require moving mold components.
If a similar visual effect can be achieved using draft-friendly geometry, tooling becomes simpler.
Injection-molding design guidance consistently identifies undercuts as an important tooling cost driver.
Use Texture Instead of Complex Geometry
Sometimes a visually rich surface can be achieved through engraving, texturing, transfer printing or coating rather than deep structural details.
Start From an Existing Base
If complete exclusivity isn’t required, ask whether the factory has an existing blank plate that can be modified.
A new logo insert or surface treatment may cost far less than building a completely new mold.
Standardize the Diameter
A dramatically oversized plate may require larger tooling and equipment.
Before finalizing the diameter, ask whether a small change could fit an existing machine or mold-base configuration.
Design for Multiple Collections
If you intend to sell several seasonal collections, develop a versatile base plate.
The same structure might support:
- Christmas patterns
- Wedding collections
- Hotel collections
- Metallic ranges
- Rustic finishes
This spreads the tooling investment across more SKUs.
The cheapest tooling quotation isn’t always the lowest-cost solution.
The goal should be efficient geometry that remains commercially attractive.
Common Tooling Problems That Delay Custom Charger Plate Projects
Many delays happen because decisions are made too late.
Changing Dimensions After Machining
A buyer approves a 330 mm diameter and later requests 350 mm.
That may sound like a small adjustment.
For the mold, it can be a major change.
Freeze critical dimensions before machining.
Approving Only Photos
Photos are useful for color discussions, but they aren’t enough for dimensional approval.
For a new mold, buyers should request physical samples whenever possible.
Late Color Changes
Changing from gold to another gold sounds easy.
It may not be.
Metallic appearance can vary because of:
- Base material
- Primer
- Coating process
- Lighting
- Surface texture
- Top coating
Approve physical color samples under realistic lighting.
Ignoring Packaging Until Production
A charger plate can pass every dimensional inspection and still arrive damaged because the carton specification wasn’t tested.
Large decorative plates need suitable protection against scratching, compression and edge impact.
Unclear Mold Ownership
This problem often appears years later.
The buyer wants to move production, but nobody knows whether the mold belongs to the customer or the factory.
Ownership must be documented before payment.
Using a Sample Without a Specification
A visual sample is helpful.
A controlled specification is better.
Record key dimensions, material, weight, color, finish and packaging requirements so repeat orders don’t depend on memory.
Who Owns the Mold and What Should Your Tooling Agreement Include?
For importers, tooling ownership is a commercial issue as much as an engineering issue.
Paying a mold fee does not automatically tell you everything about ownership.
Your purchase agreement or tooling confirmation should answer several questions.
Who Legally Owns the Tool?
If the buyer pays 100% of the tooling cost, many buyers expect ownership.
Put this in writing.
Where Will the Tool Be Stored?
Usually, it remains at the manufacturing factory because shipping a heavy mold internationally is expensive and unnecessary during normal production.
How Long Is Free Storage Provided?
Ask whether the factory has an inactivity period after which storage fees or disposal rules apply.
For comparison, some rapid-tooling services publish specific storage policies for inactive molds, which shows why buyers should not assume indefinite free storage.
Who Pays for Maintenance?
Normal maintenance and major repairs are not necessarily the same thing.
Clarify:
- Routine cleaning
- Rust prevention
- Wear-component replacement
- Major damage
- Engineering modifications
Can the Supplier Use Your Tool for Another Customer?
If you are paying for exclusive tooling, this point should be clearly stated.
Can the Mold Be Transferred?
If necessary, define whether you can request delivery of the mold and who pays freight, crating and export costs.
A mold agreement protects both sides because expectations are clear before production begins.
How Importers Should Compare Charger Plate Mold Quotations
Never compare tooling quotations using price alone.
Instead, create an apples-to-apples comparison sheet.
| Quotation Item | Supplier A | Supplier B | Supplier C |
|---|---|---|---|
| Mold cost | |||
| Mold steel | |||
| Mold base specification | |||
| Cavity number | |||
| Runner type | |||
| Expected mold life | |||
| T0/T1 sample included | |||
| Modification included | |||
| Mold lead time | |||
| Product MOQ | |||
| MOQ per color | |||
| Unit price | |||
| Decoration cost | |||
| Custom packaging MOQ | |||
| Mold ownership | |||
| Storage terms |
This table often exposes why one quotation looks cheaper.
Perhaps Supplier A quoted only basic P20-style tooling.
Supplier B included a better surface specification.
Supplier C included the first trial and revisions.
The final choice should reflect your sales plan.
A small distributor testing a new line may prioritize lower investment and flexibility.
A national retailer expecting repeat orders may prioritize stable long-term production and documented quality control.
This is also why external injection-molding benchmarks emphasize matching tooling strategy to expected production volume. Aluminum or prototype tools can make sense for lower volumes, while harder steel tooling becomes more attractive as production requirements grow.
For further technical background on injection-molding tooling, buyers can review Protolabs’ injection molding resources.
Questions to Send a Manufacturer Before Paying for Tooling
A good RFQ saves both buyer and manufacturer time.
Send as much information as possible before requesting the final tooling quotation.
Product Information
- What outside diameter do you need?
- What is the target thickness?
- Do you have a physical reference sample?
- Do you have STEP, STP, IGES or other 3D files?
- Is the shape exclusive?
Appearance
- Is the surface glossy or matte?
- Is there an embossed pattern?
- Do you need a metallic coating?
- Do you need antique finishing?
- Is a logo molded, printed or applied by label?
Commercial Requirements
- What is your first order quantity?
- What is your annual forecast?
- How many colors will you order?
- Will you reorder the same design?
Packaging
- Bulk carton?
- Individual polybag?
- Retail box?
- Barcode label?
- Private-label carton?
Tooling Requirements
Ask the supplier to state:
- Mold steel
- Cavity quantity
- Mold life expectation
- Mold ownership
- Trial procedure
- Tooling lead time
- Modification policy
Providing these details allows the manufacturer to quote an actual project rather than guessing from one reference image.
Buyer Decision Chart
Use this simple decision path before opening a new mold:
Do you need a completely exclusive shape?
↓ No
Use an existing charger plate mold
→ customize color
→ customize finish
→ customize logo
→ customize packaging
→ lower development risk
↓ Yes
Prepare drawing or reference sample
→ confirm annual forecast
→ complete DFM
→ receive tooling specification
→ approve CAD
→ manufacture mold
→ inspect T0/T1 samples
→ approve golden sample
→ begin mass production
For many new brands, beginning with an existing design is sensible.
Once sales data confirms demand, a proprietary mold can create stronger product differentiation.
Established distributors with predictable volume may choose custom tooling immediately because the cost can be spread over repeat production.
FAQs About Custom Charger Plate Molds
How much does a custom charger plate mold usually cost?
The price depends on plate diameter, geometry, mold steel, surface requirements, cavity number and planned mold life. Public plate-mold listings range from roughly a few thousand dollars upward, but a manufacturer must review the actual design before giving a dependable quotation.
What is the MOQ for a newly tooled charger plate?
The mold itself may require only one tooling set, while finished-product MOQ is separate. Production MOQ depends on injection setup, resin color, painting or plating, packaging and the manufacturer’s production schedule.
How long does it take to make a charger plate mold?
A commercial project may require roughly several weeks for engineering, machining, assembly and initial trials. Additional time should be allowed for buyer approval, mold adjustments, production, decoration and packaging before shipment.
Can I make several colors from one mold?
Yes. If the product geometry and material system remain compatible, the same mold can normally produce multiple colors. However, each color may have its own MOQ because material preparation, machine cleaning and finishing lines require separate setup.
Can one mold be used for several charger plate collections?
Yes. This is a useful strategy for B2B brands. One base shape can support different coatings, prints, textures and seasonal designs, helping you spread the tooling investment across several commercial collections.
Who owns the mold after I pay the tooling fee?
Ownership depends on your agreement with the manufacturer. Do not assume it automatically. Your purchase documentation should clearly state ownership, storage, maintenance responsibilities, exclusivity and whether the mold can be transferred to another facility.
Can the mold be changed after the first sample?
Minor corrections are often possible, depending on the mold structure and location of the change. Major dimensional or structural changes may require welding, new inserts, extensive machining or even a replacement cavity.
Should I choose the lowest mold quotation?
Not automatically. Compare steel specification, expected mold life, cavity design, trial samples, included revisions, maintenance, ownership and production efficiency. A cheaper tool can become more expensive if it causes unstable production or requires early replacement.
Do I need a custom mold just to add my logo?
Not always. Printing, labeling, transfer decoration and some logo inserts may allow customization of an existing product. A completely new mold is normally justified when you need proprietary geometry or permanent molded details.
What information should I send for an accurate quotation?
Ideally send a 3D drawing or reference sample, dimensions, material requirement, finish, estimated first order, annual demand, color quantity, logo method and packaging specification. More complete input produces a more useful tooling quotation.
Conclusion: Treat Your Charger Plate Mold as a Production Asset
A custom charger plate program should never begin with only the question, “What is your mold price?”
The more useful questions are:
- What exactly is included in the tooling?
- What mold specification fits my annual volume?
- What is the MOQ for each finish and color?
- When will the first production sample be ready?
- Who owns the tooling?
- What happens if the first sample needs modification?
- Can the same mold support future collections?
These questions move the conversation from price shopping to production planning.
For buyers, that difference matters.
A well-developed mold can support thousands of consistent products, multiple finishes and years of repeat orders. A poorly defined mold project can lead to repeated sampling, launch delays and unnecessary modification costs.
The safest approach is to complete the product definition before machining begins. Confirm dimensions, appearance, material, target volume, packaging and tooling ownership with your supplier.
Then evaluate the complete commercial picture:
tooling investment + unit cost + decoration + packaging + expected order volume + development time.
That gives you a much clearer measure of project value than the mold price alone.
NOTE: If you’re developing an exclusive charger plate for wholesale, retail, hospitality or private-label distribution, send your reference photo, CAD drawing, target dimensions, finish and expected order volume to the manufacturer’s engineering team.