Plastic Charger Plate Quality Inspection should verify appearance, dimensions, flatness, surface finishing, material consistency, decoration, packaging, quantity, and buyer-specific requirements before shipment. For bulk orders, the inspection plan should be based on an approved specification and sample. A structured sampling method can then be used to decide whether the production lot meets the agreed quality level.
For overseas buyers, a charger plate that looks simple can create surprisingly expensive problems.
A small scratch may look harmless at the factory. After plating, retail lighting can make it highly visible. Slight warpage may seem acceptable when one plate is checked. Stack 100 pieces together, though, and the problem becomes obvious.
Then there are color differences, coating defects, uneven rims, incorrect labels, weak cartons, and inconsistent packing quantities.
That’s why good QC isn’t simply about looking at finished products before loading a container. It starts before production begins.
For importers, distributors, event-supply wholesalers, retailers, and private-label brands, the goal is simple: turn subjective expectations into measurable acceptance criteria before mass production starts.
Plastic Charger Plate Quality Inspection
A reliable inspection system normally covers five stages:
Approved sample → Incoming materials → Production control → Final inspection → Packaging and shipment release
Each stage prevents a different type of risk.
Incoming material inspection helps stop incorrect resin, masterbatch, or finishing materials from reaching production. In-process inspection catches molding problems before thousands of defective pieces are produced. Final inspection checks whether finished goods match the approved specification.
Packaging inspection protects all that work during transportation.
One important lesson from charger plate manufacturing is that appearance needs more control than many buyers initially expect.
A charger plate is highly visual. Large decorative surfaces reflect light easily. Metallic finishes make scratches, dust marks, fingerprints, uneven coating, and color variation easier to notice.
The specification should therefore define more than diameter and color.
A useful QC specification normally includes:
- Product diameter and height
- Product weight or approved weight range
- Material requirement
- Referencia de colores
- Acabado superficial
- Logo or decoration position
- Flatness requirement
- Rim shape
- Acceptable visual defects
- Packaging method
- Label and barcode information
- Carton quantity
- Buyer-specific tests
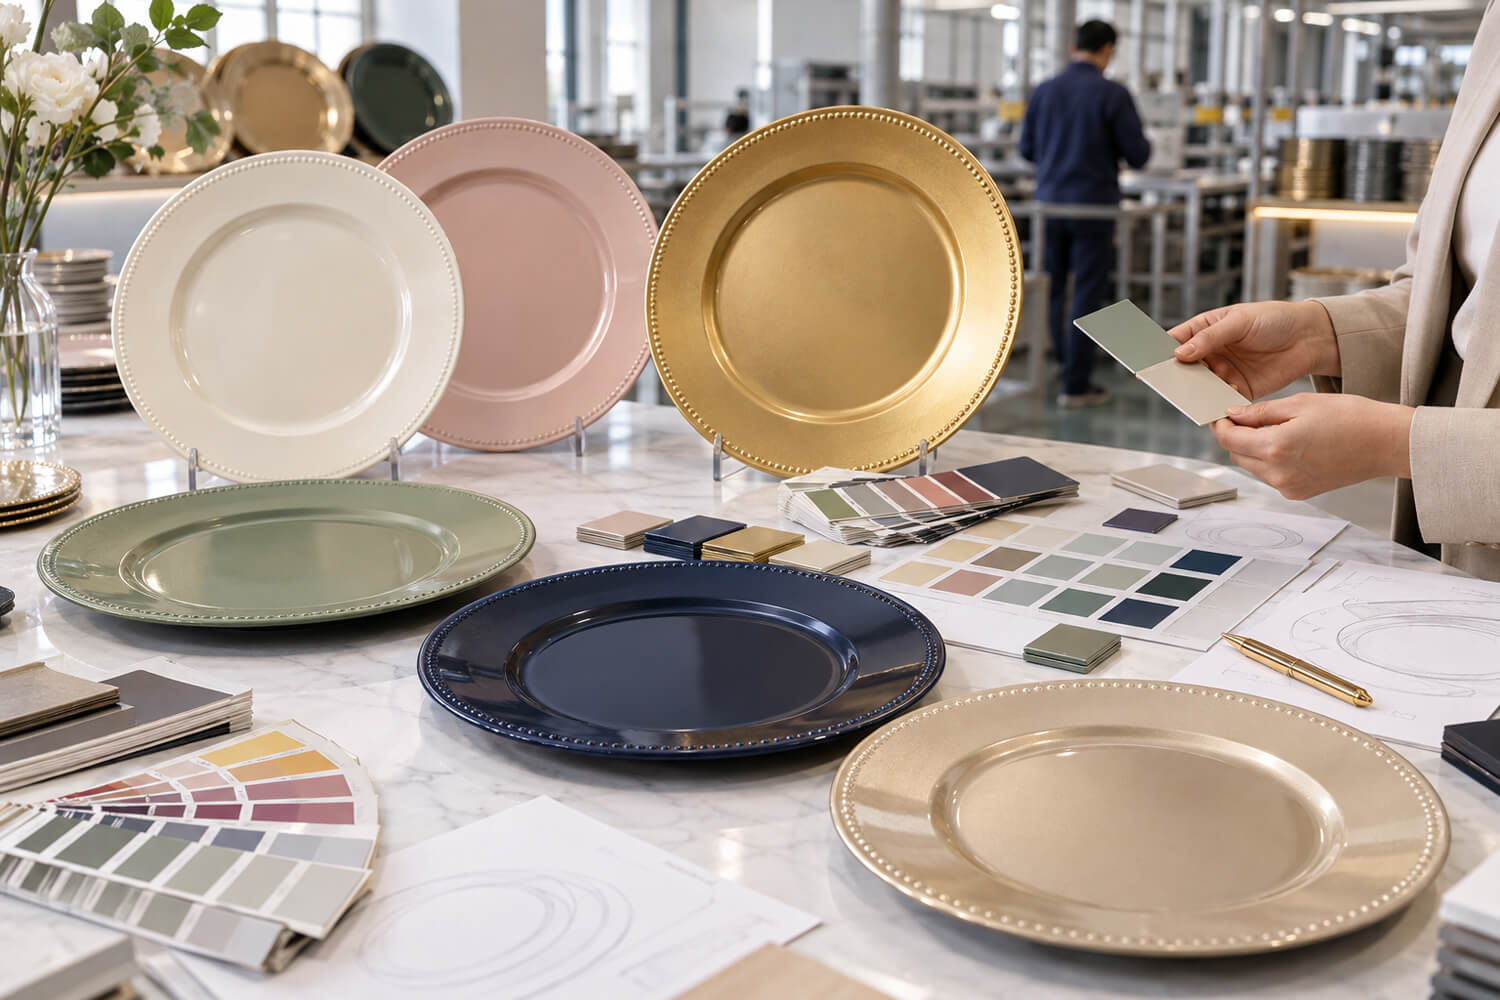
The approved reference sample is especially important.
Photos alone aren’t enough for metallic gold, silver, rose gold, pearl, matte, or special-effect finishes. Camera settings and screen displays can change how the color looks.
For those finishes, a physical signed sample or agreed instrumental color standard gives both buyer and manufacturer a clearer reference.
Start With an Approved Quality Standard Before Production
The most effective inspection starts before the first production piece comes out of the mold.
Before mass production, the buyer and manufacturer should agree on what an acceptable product actually is.
This sounds obvious. Yet many quality disputes begin because both sides use words such as “good quality,” “no scratches,” or “same as sample.”
Those descriptions aren’t precise enough.
For example, what counts as a scratch?
A tiny mark visible only under strong inspection lighting is very different from a 20 mm scratch visible immediately on a retail shelf.
A practical pre-production quality file should contain:
| Quality Item | Recommended Reference |
|---|---|
| Product shape | Approved sample or drawing |
| Diameter and height | Technical specification |
| Color | Physical color sample, Pantone reference, or agreed color data |
| Acabado superficial | Signed production sample |
| Artwork | Approved digital artwork |
| Ubicación del logotipo | Dimensioned artwork or sample |
| Peso del producto | Agreed range where relevant |
| Embalaje | Approved packing specification |
| Carton marks | Confirmed shipping mark artwork |
| Código de barras | Buyer-approved barcode file |
| Defect limits | Written inspection criteria |
Revision control matters too.
If a buyer changes the gold tone after the first sample, the old sample shouldn’t remain beside the production line. The final approved version should carry a clear date or revision number.
That small step prevents a surprising number of disputes.
For private-label programs, we also recommend treating product approval and packaging approval as separate checkpoints. A correct plate packed with the wrong barcode or carton marking can still create a serious warehouse problem.
Raw Material and Incoming Material Inspection
Quality can’t be inspected into a finished product if the starting materials are already wrong.
Plastic charger plates may use different polymers depending on the required design, manufacturing process, finish, price target, and intended use.
Incoming quality control should therefore verify materials against the purchase specification instead of relying only on appearance.
Typical checks include:
- Resin grade or material identification
- Supplier batch information
- Masterbatch color
- Recycled-material requirement, when applicable
- Coating or paint identification
- Printing ink or decoration material
- Packaging materials
- Supplier certificates when contractually required
For repeat orders, material consistency matters just as much as material type.
Changing resin grade, pigment concentration, or coating supplier can alter gloss, molding behavior, shrinkage, color, plating performance, and product stiffness.
That’s why traceability is useful.
A factory should be able to connect a finished production batch with the materials used for that batch. If a problem appears later, the manufacturer can investigate which resin, masterbatch, paint, coating, or production run was involved.
Material documents shouldn’t replace physical inspection, however.
A certificate may confirm what was ordered. It doesn’t prove that every finished plate is dimensionally correct or visually acceptable.
The strongest system combines:
supplier documentation + incoming inspection + production monitoring + finished-product verification
For B2B buyers, this provides more useful protection than asking only whether a supplier has “QC.”
Injection Molding Quality Control During Production
Waiting until production is complete is expensive.
If a molding problem begins during the first hour and nobody notices it until final inspection, thousands of pieces may require sorting or reworking.
In-process inspection is designed to prevent that situation.
Common molding defects on plastic charger plates may include:
- Short shots
- Excessive flash
- Sink marks
- Marcas de flujo
- Weld lines
- Black spots
- Contamination
- Gate marks
- Uneven rim formation
- Surface dents
- Warpage
- Cracks
- Abnormal shrinkage
Not every visible molding line is automatically a reject. Acceptance depends on the approved specification, finish, visibility, and intended market.
The key is consistency.
Operators and QC staff should compare production against the approved sample at defined intervals. Dimensional checks should also be repeated during the production run.
Product weight can be a useful process indicator.
If the same molded product suddenly becomes noticeably lighter, it may indicate a molding or material change. However, weight alone doesn’t prove that a product is acceptable.
Diameter, flatness, wall formation, appearance, and finish still need separate verification.
Another practical point is cavity consistency.
When a mold has multiple cavities, products from different cavities should be compared. One cavity may produce a recurring defect while the others remain acceptable.
Cavity-based defect tracking helps the molding team identify problems much faster than mixing all defective parts together.
Surface Finish, Plating, Painting and Decoration Inspection
Surface finishing is often the most sensitive stage of charger plate QC.
Metallic plating and decorative coatings can make the product attractive, but they also make inconsistencies easier to see.
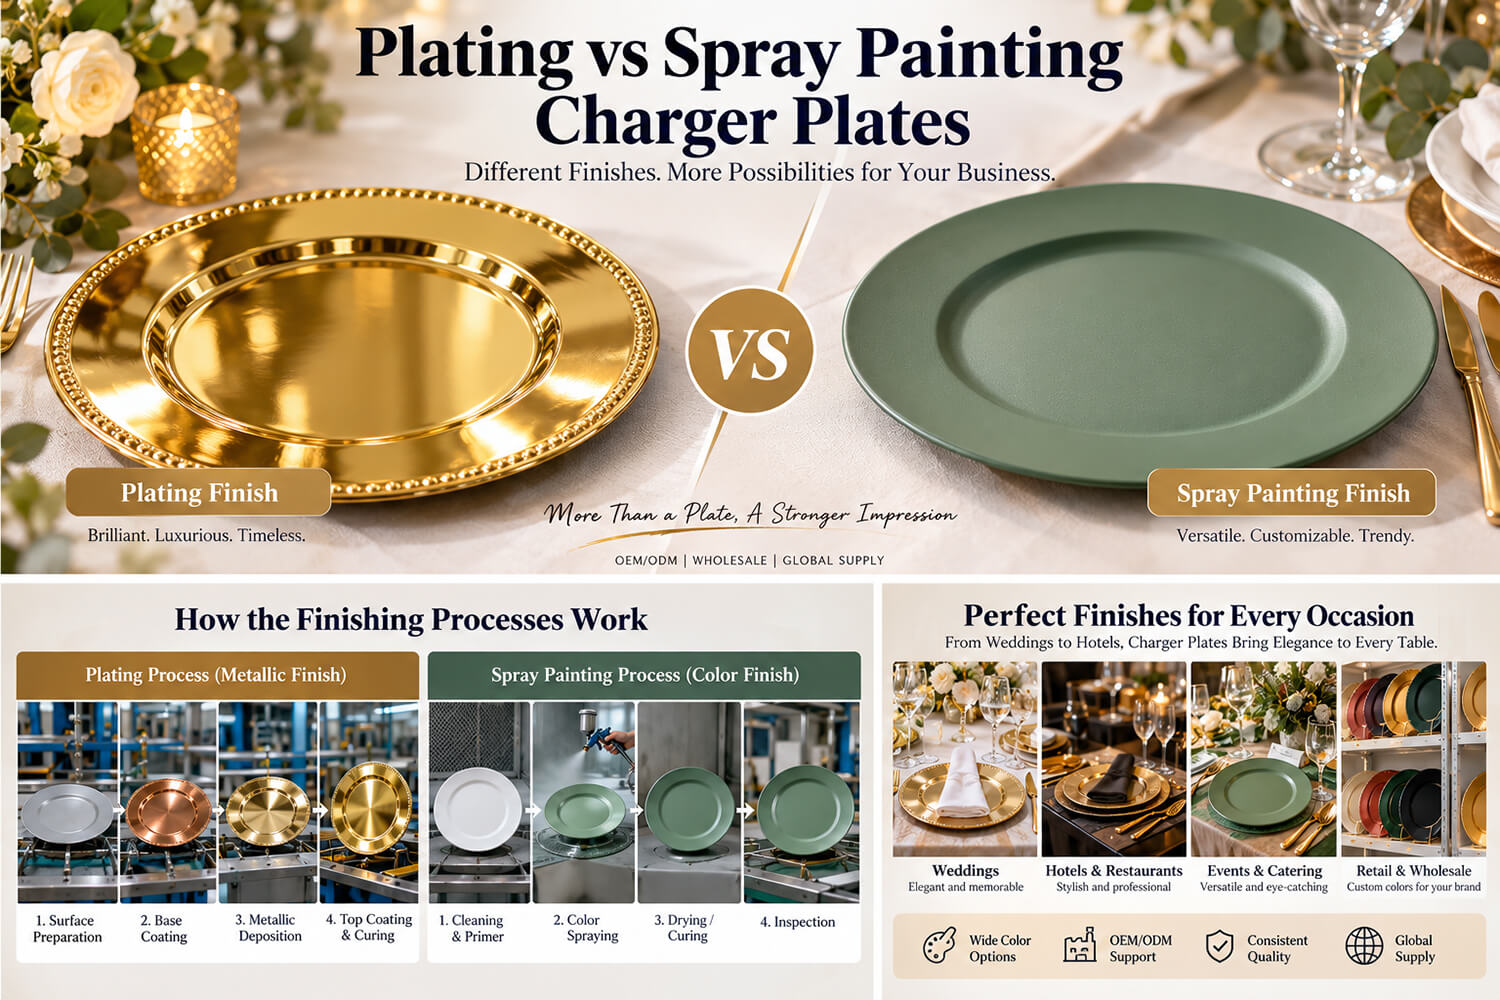
For plated products, inspection commonly focuses on:
- Uniformidad del color
- Uneven metallic effect
- Missing coating
- Dark spots
- Burn marks
- Pinholes
- Edge coverage
- Scratches
- Fingerprints
- Surface contamination
- Peeling or weak adhesion
Spray-painted finishes require slightly different attention.
QC should look for dust particles, orange peel, excessive paint, thin coverage, runs, pinholes, tackiness, overspray, and inconsistent gloss.
Printed or decorated products may require checks for:
- Artwork position
- Logo orientation
- Color
- Registration
- Missing print
- Blurred edges
- Bubbles
- Wrinkles
- Decal lifting
- Incorrect artwork version
Color control deserves special attention.
A visual comparison under controlled lighting is useful. For tighter private-label programs, a spectrophotometer can provide objective color data.
Instead of simply writing “color must be the same,” buyers can agree on a measurable color-difference limit when necessary.
The exact limit should be established for the specific finish and approved standard. Metallic surfaces can behave differently from solid-color molded plastic.
Adhesion testing can also be specified for painted or coated products.
The test method, conditioning time, tape type, cut method, and pass criteria should be agreed before production. Standards such as ISO 2409 or ASTM D3359 may be used when appropriate to the coating system and contract.
Llamada a la acción sutil: If you’re developing a custom charger plate finish, send the target sample, Pantone reference, artwork, and packaging requirement to the manufacturer before quotation. That makes the quotation and quality standard much more accurate.
Dimensions, Weight, Flatness and Stackability Checks
A plate can look beautiful and still create problems in use.
That is why dimensional inspection shouldn’t be skipped.
Typical measurements include:
| Parameter | Inspection Method | Por qué es importante |
|---|---|---|
| Outer diameter | Caliper or approved gauge | Fit, appearance and set consistency |
| Overall height | Caliper / height gauge | Table presentation and stacking |
| Ancho de la llanta | Caliper or template | Visual consistency |
| Peso del producto | Digital scale | Coherencia del proceso |
| Planicidad | Flat reference surface / agreed gauge | Prevents rocking |
| Ubicación del logotipo | Ruler, fixture or template | Branding consistency |
| Alineación de los elementos decorativos | Template / visual reference | Retail appearance |
| Cantidad por embalaje | Count or weight-supported verification | Shipment accuracy |
Flatness is especially important.
A small amount of deformation may not be obvious while holding a plate. Place it on a flat table and the problem becomes much easier to detect.
A warped charger can rock or sit unevenly.
Stackability should also be checked.
Products may pass an individual appearance inspection yet nest badly when stacked. This can increase carton height, create pressure points, cause scratches, or reduce loading efficiency.
For large orders, simple go/no-go fixtures can speed up repetitive dimensional inspection.
The exact tolerance should come from the approved drawing or quality specification.
Manufacturers shouldn’t invent a universal tolerance for every charger plate. A simple molded design and a highly decorative plated plate may require different control points.
This buyer-specific approach is more reliable than using one generic standard across every design.
Appearance Defect Classification for Bulk Orders
Visual defects need classification because not every defect has the same commercial impact.
A useful inspection system normally separates defects into critical, major, and minor categories.
| Defect Class | Practical Meaning | Possible Charger Plate Examples |
|---|---|---|
| Critical | Safety, legal, or serious compliance risk | Dangerous sharp edge, prohibited material where applicable |
| Major | Likely to cause rejection, complaint, or loss of intended use | Large scratch, severe warpage, peeling coating, wrong color, wrong logo |
| Minor | Small defect that doesn’t materially affect normal use | Small cosmetic mark within agreed limit |
The exact classification belongs in the buyer’s inspection specification.
For example, a visible scratch on the center display area may be classified differently from a tiny mark on the bottom.
Viewing conditions matter too.
If inspectors examine shiny metallic plates from five centimeters away under extremely intense lighting, they may identify marks that normal customers would never see.
On the other hand, inspecting quickly in a dark warehouse can allow obvious defects to pass.
A good specification can define:
- Viewing distance
- Lighting conditions
- Inspection time
- Primary visible surface
- Secondary surface
- Maximum defect size
- Maximum defect quantity
This reduces subjective decisions.
It also helps the factory train inspectors consistently.
For private-label retail products, cosmetic standards are often more demanding because shoppers evaluate the product visually before use.
Wholesale event-supply programs may prioritize consistency, stackability, finish durability, and transport protection.
The inspection standard should reflect the actual sales channel.
Functional and Regulatory Checks Based on Intended Use
One of the biggest mistakes in product QC is testing every product against assumptions instead of its intended use.
Start by defining what the charger plate is designed to do.
Is it decorative?
Will food contact it directly?
Is it reusable?
Is dishwasher resistance claimed?
Will the plate be exposed to hot food?
Will it be used mainly for weddings, restaurants, rental companies, or retail decoration?
Those questions determine the testing requirement.
If a plastic article is specifically intended and marketed for direct food contact, its materials and intended conditions of use need appropriate regulatory review.
In the United States, FDA explains that food-contact substances used in food-contact materials must have appropriate authorization for their intended use. The intended food type and conditions of use are relevant to that assessment. citeturn431484search0turn431484search10
FDA Food Contact Substance Information
For the European Union, Regulation (EU) No 10/2011 applies to plastic materials and articles intended to come into contact with food. The regulation has been amended over time, so exporters should confirm the current consolidated requirements for the destination market and intended use. citeturn431484search13
EU Regulation on Plastic Food Contact Materials
The lesson for buyers is important:
Don’t ask only, “Is this food safe?”
Instead ask:
- What is the intended use?
- Which material is used?
- Is direct food contact claimed?
- Which destination market applies?
- Which test report supports that specific product or material?
- Does the coating or decoration affect the compliance requirement?
That produces a much more useful answer.
AQL Sampling and Final Random Inspection
Large production lots are rarely inspected piece by piece during independent final random inspection.
Instead, buyers often use statistical sampling.
As of 2026, the current ISO standard for AQL-indexed lot-by-lot attribute inspection is ISO 2859-1:2026. It was published in January 2026 and replaced the previous 1999 edition. The standard provides single, double, and multiple sampling schemes and includes rules for different inspection conditions. citeturn999097view0
ISO 2859-1:2026 Official Standard Page
A practical inspection specification might state something such as:
General Inspection Level II, with buyer-defined AQL limits for major and minor defects.
Some consumer-goods programs use values such as:
- Critical defects: zero acceptance in the inspected sample
- Major defects: AQL 2.5
- Minor defects: AQL 4.0
These values are examples, not universal rules.
The buyer should choose the inspection level and acceptance limits according to product risk, market expectations, supplier performance, and contractual requirements.
AQL also doesn’t mean that a buyer is deliberately accepting that exact percentage of defective goods in every shipment.
It is part of a statistical lot-acceptance system.
The actual sample size and acceptance/rejection numbers depend on the lot, inspection level, chosen AQL, and sampling plan.
That distinction matters.
AQL is useful for making consistent shipment decisions. It shouldn’t replace good process control.
Example Final Inspection Flow
Finished production
↓
Confirm lot quantity
↓
Randomly select cartons
↓
Randomly select product samples
↓
Check workmanship and specifications
↓
Classify defects
↓
Apply agreed sampling criteria
↓
Check packaging and quantity
↓
PASS / HOLD / REWORK / RE-INSPECT
A failed inspection shouldn’t automatically mean the entire order goes into the trash.
The factory can identify the cause, conduct sorting or rework where appropriate, document corrective action, and present the corrected lot for re-inspection.
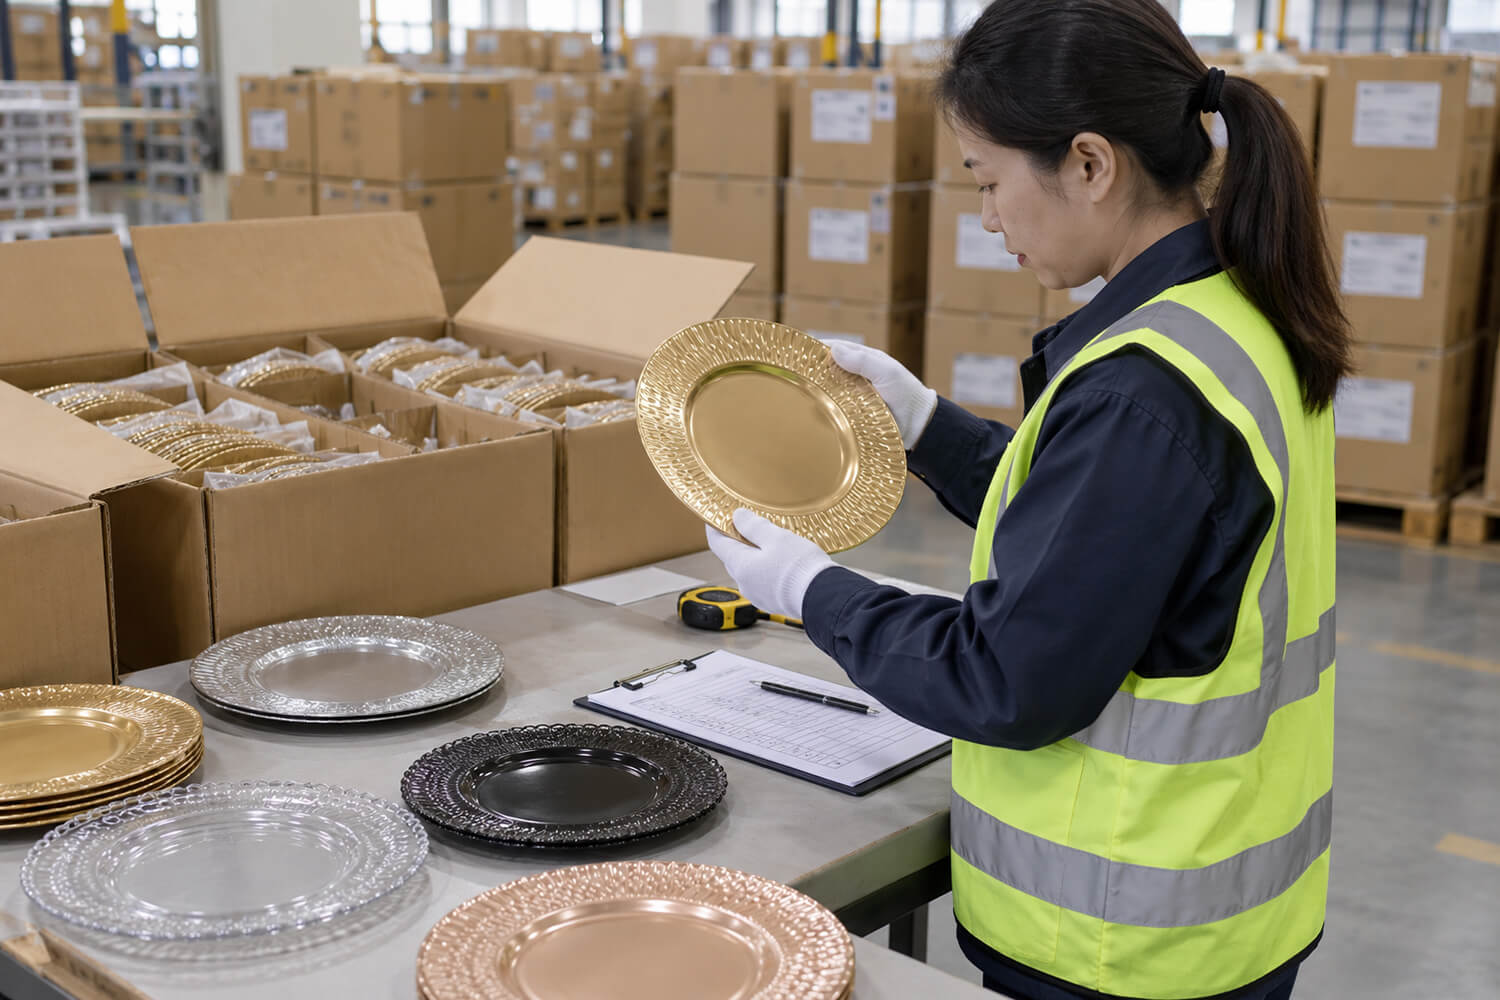
Packaging Inspection Before Shipment
Good products can become bad products during transportation.
For charger plates, packaging deserves particular attention because decorative surfaces can scratch when plates rub against each other.
The packaging system should protect both the product and the finish.
Typical inspection points include:
- Individual protective bag where required
- Protective film or separator
- Correct stacking direction
- Inner-box quantity
- Master-carton quantity
- Barcode accuracy
- Shipping marks
- Country-of-origin marking where required
- Dimensiones de la caja
- Gross and net weight
- Carton closure
- Moisture protection where necessary
- Pallet configuration when applicable
Metallic and high-gloss finishes may need extra separation.
If two decorated surfaces rub repeatedly during sea transport, a plate that passed factory inspection may arrive scratched.
Packaging should therefore be validated with the actual finish.
Another common problem is carton overloading.
Putting more plates into each carton may reduce carton count. However, excessive weight can increase carton deformation and product pressure.
There is a balance between shipping efficiency and protection.
For demanding projects, the buyer may specify a packaging performance or transit test. The exact test should match the distribution environment.
Retail packaging also needs separate verification.
A perfect charger plate inside a box with the wrong barcode, color sticker, SKU, or quantity is still a shipment problem.
That’s why final QC should treat product quality and packaging accuracy as two separate pass conditions.
Quality Records, Traceability and Corrective Action
A professional QC system should produce evidence.
For B2B buyers, quality records become especially valuable when orders are repeated over several seasons.
Useful records include:
- Inspección de la mercancía recibida
- Production batch number
- In-process inspection records
- Finished-product inspection
- Defect photographs
- Measurement records
- Inspección de envases
- Approved samples
- Artwork revisions
- Corrective-action records
- Re-inspection results
Traceability makes problem solving faster.
Suppose one shipment contains gold plates with an unusual color difference.
Without batch records, the investigation becomes guesswork.
With traceability, the manufacturer may be able to compare production dates, coating batches, material lots, equipment settings, inspectors, and retained samples.
Corrective action should also go beyond sorting defective pieces.
A useful investigation asks:
What happened?
Why did it happen?
Why wasn’t it detected earlier?
How will recurrence be prevented?
This distinction separates temporary rework from real process improvement.
For example, operators can sort scratched plates before shipment. That fixes the current order.
But if scratches were caused by plates touching during transfer, the long-term solution may involve changing trays, separators, handling methods, or workstations.
That’s where quality management creates value for repeat B2B orders.
Buyer Quality Checklist Before Approving Shipment
Before approving a bulk shipment, buyers can use a short checklist to make sure important requirements haven’t been overlooked.
Producto
- Does the product match the approved sample?
- Is the material correct?
- Are dimensions within the agreed specification?
- Is the plate stable on a flat surface?
- Is the rim shape consistent?
- Is product weight within the agreed range where specified?
Aspecto
- Is the color correct?
- Is the gloss or metallic effect consistent?
- Are scratches within agreed limits?
- Are coating defects acceptable?
- Are edges clean?
- Is decoration positioned correctly?
Imagen de marca
- Is the correct logo used?
- Is artwork the latest approved version?
- Are labels correct?
- Are barcodes readable?
Embalaje
- Is the quantity per inner box correct?
- Is the carton quantity correct?
- Are surfaces protected?
- Are shipping marks correct?
- Are cartons strong enough for the planned shipment?
Documentation
- Is the inspection report complete?
- Are required test reports available?
- Are production and material records traceable?
- Have previous corrective actions been closed?
The checklist should be customized for the product.
A simple solid-color PP charger may not need the same finishing controls as an electroplated charger with custom logo decoration.
That’s exactly why a buyer-specific QC file is so valuable.
PREGUNTAS FRECUENTES
What should be checked during charger plate inspection?
Inspection should cover material, dimensions, flatness, color, surface finish, scratches, molding defects, logo or decoration, product quantity, packaging, labels, and buyer-specific functional requirements. The final checklist should follow an approved specification rather than subjective judgment.
What AQL should be used for plastic charger plates?
There is no universal AQL for every order. A buyer may use an inspection plan such as General Inspection Level II with separately defined limits for major and minor defects. The correct level depends on risk and purchasing requirements.
Should every charger plate be inspected?
Not necessarily. In-process controls may include frequent or targeted checks, while final random inspection often uses statistical sampling. Critical production stages may justify additional screening or 100% sorting when the defect risk is high.
How do you inspect metallic charger plate finishes?
Inspect color consistency, plating coverage, scratches, spots, fingerprints, pinholes, edge finish, gloss variation, peeling, and visible surface defects. Physical reference samples and controlled lighting are especially useful for gold, silver, and other reflective finishes.
How can buyers control color differences between production batches?
Keep an approved physical sample and define lighting or instrumental color requirements where necessary. For repeat orders, compare new production with retained reference samples and monitor material, pigment, coating, and process changes that may affect color.
Are plastic charger plates automatically food safe?
No assumption should be made from the product name alone. Requirements depend on material, coating, decoration, intended use, food-contact conditions, and destination market. Direct food-contact claims should be supported by appropriate regulatory and testing documentation.
Why is flatness important for charger plates?
Excessive warpage can cause a plate to rock on the table, stack poorly, create uneven presentation, or increase scratches during packing. Flatness should therefore be included in the agreed dimensional and functional inspection criteria.
What documents should a charger plate manufacturer provide before shipment?
Depending on the order, buyers may request an inspection report, packing list, approved specification, material or compliance documentation, test reports, production records, defect photographs, and corrective-action records. Documentation requirements should be confirmed before production.
Conclusión
Consistent Plastic Charger Plate Quality Inspection is not one final check at the end of production.
It begins with a clear specification and approved sample. It continues through incoming materials, molding, finishing, dimensional control, packaging, and final random inspection.
For B2B buyers, this approach reduces several common risks:
- Inconsistent colors
- Visible scratches
- Plating defects
- Warped products
- Incorrect artwork
- Wrong packaging
- Shipment quantity errors
- Repeated quality complaints
For manufacturers, the same system reduces rework and makes repeat orders easier to manage.
Most importantly, good QC replaces vague expectations with measurable standards.
Before your next bulk order, provide the manufacturer with your product specification, approved sample, color requirement, artwork, packaging details, destination market, and inspection criteria.
NOTE: If you’re sourcing custom plastic charger plates for wholesale, retail, distribution, or private-label programs, send your target design, reference sample, color, quantity, packaging requirements, and destination market to our team. We can review the specifications and prepare a manufacturing and quality-control proposal for your project.