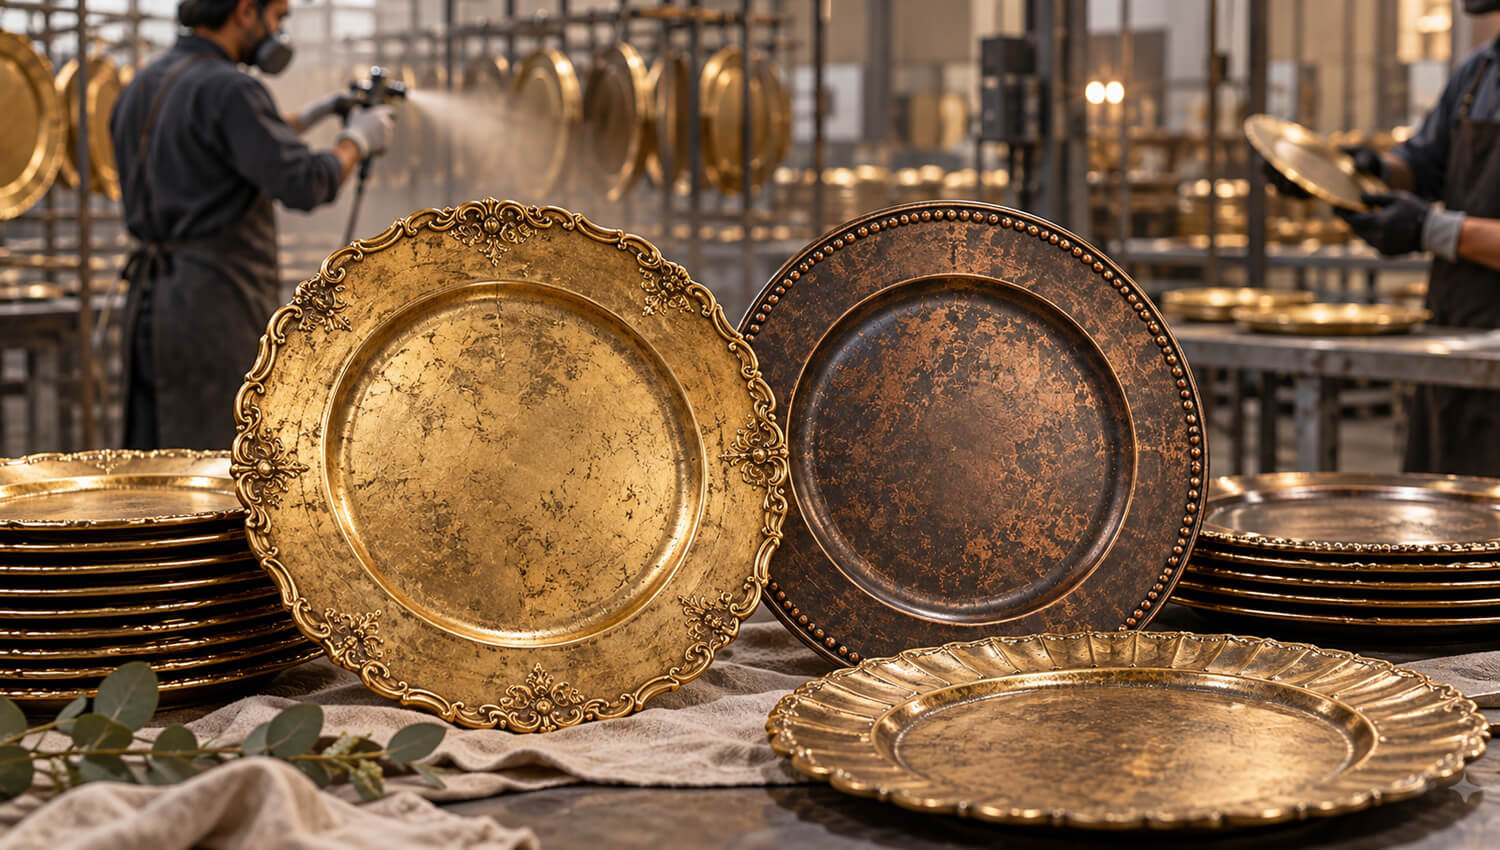
Antique Finish Charger Plates are normally made by molding the plate body, preparing its surface, applying a metallic base color, adding a darker antiquing layer, selectively removing or blending that layer, and finally applying a protective coating. The process creates highlights on raised areas and darker tones inside grooves, giving an ordinary molded plate the visual depth of aged metal.
The real challenge is repeatability.
A beautiful showroom sample isn’t very useful when 20% of the production order arrives noticeably darker than the approved piece. Hotels, event rental companies, wedding suppliers, distributors, and tableware brands usually need hundreds or thousands of pieces to look reasonably consistent when they’re placed together.
That makes the production method important.
A good factory shouldn’t simply say, “We can make antique gold.” It should be able to explain what antique gold means in that specific project. There should be an approved reference showing the base color, darkening intensity, highlighted areas, gloss level, and acceptable natural variation.
Unlike a solid-color product, an antique finish deliberately contains variation. That’s part of its appeal. The objective isn’t to eliminate variation completely. The objective is to make variation controlled and intentional.
From a manufacturing point of view, a typical decorative charger plate passes through several stages:
molding → trimming → cleaning → base preparation → metallic color → antiquing → protective coating → curing → inspection → packing
Each stage affects the final appearance.
A molding defect may become more visible after metallic coating. Poor cleaning may cause coating failure. Too much dark glaze can make the plate look dirty instead of aged. Too little can make it look like normal metallic paint.
For buyers, the safest approach is therefore to approve the complete finishing system, rather than choosing a color from a small digital photograph.
Choosing the Right Charger Plate Base Material
The antique appearance begins with something buyers rarely see: the substrate underneath the decoration.
For decorative event charger plates, molded plastics are widely used because they allow detailed rim patterns, relatively low weight, repeatable dimensions, and efficient mass production. The exact resin should be confirmed with your supplier because materials vary by product design, price level, intended application, and required performance.
The substrate influences more than cost.
It can affect rigidity, weight, molding detail, coating adhesion, impact performance, surface smoothness, and how metallic coatings appear under light.
A deeper decorative rim, for example, creates more shadow after antiquing. A smooth flat rim produces a much more restrained aged-metal effect.
| Omil | What the Buyer Should Evaluate | Nega bu muhim |
|---|---|---|
| Plataning diametri | Actual measured size | Must match table-setting requirements |
| Og'irlik | Piece weight and tolerance | Influences perceived quality and shipping cost |
| Qattiqlik | Flexing under normal handling | Important for rental and event use |
| Rim depth | Height and profile | Changes visual character |
| Embossing detail | Sharpness of molded pattern | Determines how well antiquing highlights details |
| Yuzaning sifati | Sink marks, flow marks, scratches | Metallic finishes can reveal imperfections |
| Back construction | Rib design and support | Influences stability and stacking |
One lesson manufacturers learn quickly is that a decorative finish can’t rescue poor molding.
Metallic surfaces reflect light strongly. Tiny flow lines, sanding marks, scratches, or uneven surfaces may become easier to see after coating.
That’s why buyers developing a custom design should review an uncoated molding sample as well as the finished sample when tooling is involved.
For existing factory molds, this isn’t normally necessary for every order. But when you commission a new rim pattern, unusual diameter, logo, or embossed design, reviewing the raw molded part helps catch tooling issues before decorative processing begins.
You should also tell your supplier how the product will actually be used. A wedding décor distributor, hotel supplier, and event rental company may have different priorities for appearance, durability, packaging, and repeated handling.
Molding the Plate and Creating Decorative Details
Once the material and design are confirmed, the body of the charger plate is formed.
For molded plastic designs, the geometry of the tool determines much of the final visual character. The center diameter, rim width, decorative pattern, edge profile, reinforcement ribs, and surface texture are built into the mold.
This matters especially for antique styles.
Think about an old bronze picture frame. Its aged character is more obvious because dark coloration settles around recessed details while raised areas remain brighter. Charger plates work in much the same way.
Patterns such as beads, hammered textures, carved borders, geometric motifs, floral reliefs, and irregular organic textures give the finishing process somewhere to create contrast.
A completely flat surface gives the factory fewer opportunities to build that natural-looking depth.
During molding, operators and inspectors normally watch for problems such as:
- Short filling or incomplete details
- Warpage
- Obvious gate marks
- Flash around edges
- Chuqur izlar
- Surface contamination
- Scratching during handling
- Inconsistent dimensions
These issues shouldn’t simply be covered with more paint.
A poorly defined decorative rim will still look poorly defined after antiquing. In fact, darker glaze may emphasize the defect.
For OEM projects, buyers should therefore separate design approval dan color approval.
First determine whether the molded shape itself is acceptable. Look at the decorative pattern from several angles and under side lighting. Run your fingers across the edge. Stack several samples. Check whether the plate sits flat.
Then approve the finishing treatment.
This two-stage approach may seem slower during development, but it can prevent far more expensive changes once production begins.
For existing molds, buyers can usually shorten the process significantly. The main development work then moves from tooling to finish sampling: antique gold, antique silver, bronze, copper, champagne, black-gold, or another requested appearance.
Preparing the Surface Before Decorative Coating
Surface preparation isn’t the glamorous part of production, but it can be one of the most important.
Before decorative coating is applied, the molded surface should be suitable for the selected coating system. Dust, oil, mold-release residue, handling contamination, or loose particles can interfere with the finish.
Think of painting a dusty wall. Even expensive paint won’t perform properly if the surface underneath isn’t ready.
Industrial surface preparation depends on the resin and coating chemistry being used, so buyers shouldn’t assume that every manufacturer follows one identical formula.
Typical production controls can include cleaning, dust removal, controlled handling, suitable pretreatment, and primer where the coating system requires it.
The objective is straightforward:
the decorative layers must bond consistently to the substrate.
This is also where buyers should distinguish between visual inspection and performance verification.
A freshly coated sample can look excellent even if the coating system isn’t robust enough for repeated handling. For larger orders or demanding commercial applications, buyer and supplier can agree on suitable adhesion or abrasion checks.
ASTM D3359, for example, describes tape-test methods used to assess coating adhesion. ASTM itself notes important limitations and substrate considerations, so it shouldn’t automatically be presented as a universal pass/fail requirement for every plastic charger plate. It can, however, provide a useful starting point when buyer and manufacturer are establishing a mutually agreed coating test.
For further reference, buyers can review the official standard information from ASTM International: ASTM D3359 — Standard Test Methods for Measuring Adhesion by Tape Test.
From a purchasing perspective, the important question isn’t simply, “Do you test the coating?”
Ask instead:
What test do you perform, on which surface, using what acceptance criteria, and is that requirement written into my order specification?
That question produces far more useful answers.
Building the Metallic Base Color
The metallic layer gives an antique charger plate its underlying visual identity.
Before it looks old, it generally needs to look metallic.
Depending on the product design and factory process, manufacturers may use decorative coating systems that create gold, silver, bronze, copper, champagne, pewter, or other metal-inspired appearances.
The exact finishing route can vary substantially between suppliers. Buyers shouldn’t assume that every “antique gold” product uses the same paint, deposition process, layer thickness, or topcoat chemistry.
What matters commercially is whether the resulting finish meets the agreed master sample and performance requirements.
For an antique gold design, for example, the base may begin relatively bright. The later antiquing process reduces that brightness in selected areas.
That creates contrast:
| Base Appearance | Antiquing Treatment | Typical Visual Result |
|---|---|---|
| Bright gold | Light brown shading | Warm vintage gold |
| Yellow gold | Dark brown shading | Traditional antique gold |
| Shampan | Soft brown/gray shading | Subtle luxury appearance |
| Kumush | Charcoal shading | Antique silver |
| Copper | Brown/black shading | Aged copper |
| Bronze | Dark brown shading | Classic old-bronze appearance |
Notice that “antique gold” isn’t one objective color.
One customer may expect something close to aged brass. Another may expect a warmer wedding gold with only slight dark shading. A third may want an intentionally distressed finish with strong black accents.
That’s why factory teams shouldn’t rely only on names.
The safest OEM method is to work from a physical approved sample whenever color interpretation matters.
Photos are useful during early development, but screens, cameras, lighting, editing, and compression all change color appearance.
For large repeat orders, retaining signed or labeled master samples gives both sides a much clearer reference.
When your purchasing team requests a quotation, send the intended visual reference at the RFQ stage. The manufacturer can then determine whether the desired appearance fits an existing finish or requires a new sample-development cycle.
Creating the Antique and Distressed Effect
This is the stage that turns an ordinary metallic charger plate into something visually older and more dimensional.
A darker decorative layer is introduced over, into, or around the metallic appearance. Depending on the chosen production system, that dark material can then be blended, wiped, sprayed, brushed, rubbed, or otherwise controlled so more shading remains in selected areas.
Raised points stay brighter.
Grooves become darker.
Edges may receive additional depth.
The result resembles natural aging because real objects rarely age uniformly.
For decorative charger plates, this contrast is especially effective on detailed rims. Beaded borders, embossed patterns, irregular textures, and carved-style designs naturally catch the darker layer.
But this stage creates one of the biggest manufacturing challenges: how much variation is acceptable?
An antique treatment shouldn’t look mechanically identical on every square millimeter. If it does, the product can lose the handmade visual quality buyers want.
Yet unrestricted variation isn’t acceptable either.
Suppose 100 plates are arranged at a wedding reception. If half look light champagne and the rest look nearly brown, guests may see them as different products.
A well-controlled production order therefore needs a visual range.
In practical factory development, the approved sample should establish several characteristics:
overall color family, darkness level, highlight intensity, treatment around the rim, treatment inside decorative recesses, gloss level, and acceptable variation.
For high-value programs, a buyer can approve several boundary samples rather than one perfect sample.
One represents the lightest acceptable appearance.
Another represents the darkest acceptable appearance.
A middle sample represents the preferred standard.
This is particularly useful for distressed and antiqued products because it converts a subjective phrase such as “a little darker” into something production inspectors can actually compare.
It also makes communication much easier when orders are repeated months later.
Protecting Antique Finish Charger Plates With a Topcoat
After the visual effect is created, the decorative system may require a protective clear or finishing layer.
The purpose isn’t merely gloss.
A suitable topcoat can help protect the decorative layers from handling, rubbing, packing contact, and other stresses expected during the intended use of the product.
The finish must then be cured according to the coating system before the pieces are handled aggressively or packed.
This stage is particularly relevant for B2B buyers because charger plates often pass through far more handling than consumers realize.
A plate may be produced, inspected, stacked, sleeved, packed, transported, unpacked by a distributor, repacked, delivered to an event venue, handled by staff, cleaned, stored, and used again.
Each step creates opportunities for abrasion.
ASTM D4060 is one recognized method for evaluating abrasion resistance of organic coatings on rigid surfaces using a Taber Abraser. ASTM describes the method as useful for evaluating coating abrasion resistance, while also noting factors that affect test results. Whether this method is appropriate for a specific charger plate system should be agreed between the buyer, coating supplier, laboratory, and manufacturer rather than assumed automatically.
Official information is available here: ASTM D4060 — Abrasion Resistance of Organic Coatings.
For many commercial projects, buyers don’t necessarily need to demand expensive laboratory testing on every shipment.
They do need a rational durability specification.
That specification might combine visual inspection with agreed internal rub, adhesion, packing, or handling checks. More demanding applications can add third-party testing where justified.
One point deserves special attention: decorative charger plates aren’t automatically dinner plates.
Unless a product is specifically designed, tested, and documented for direct food contact, buyers should market and use it according to the manufacturer’s stated intended application.
Never assume food-contact suitability merely because the product looks like tableware.
Controlling Color and Finish Consistency in Mass Production
For professional buyers, this may be the most important section in the entire guide.
Creating one attractive sample isn’t difficult.
Creating thousands of pieces that stay inside an agreed appearance range is the real manufacturing job.
The process should begin with a confirmed master sample. That reference needs to remain accessible to production and inspection teams during manufacturing.
Color consistency can then be influenced by several factors, including coating preparation, application amount, operator technique, equipment settings, curing conditions, antiquing intensity, and inspection lighting.
Antique effects add another complication: some intentional irregularity is desirable.
This means traditional “same color everywhere” thinking doesn’t always work.
A practical specification can separate the finish into measurable or visually comparable characteristics.
| Control Point | What to Confirm |
|---|---|
| Base metallic tone | Matches approved reference |
| Antique darkness | Within approved visual range |
| Highlight distribution | No obviously unfinished areas |
| Decorative grooves | Darkening visible and reasonably consistent |
| Gloss | Comparable to master sample |
| Overspray / contamination | Not visible from normal inspection distance |
| Peeling / coating failure | Not acceptable |
| Severe scratches | Not acceptable |
| Batch appearance | Pieces look harmonious when grouped together |
For larger orders, random pieces should also be viewed together, not only one at a time.
Nega?
Because variation that looks harmless when inspecting one plate may become obvious when 20 plates are placed side by side.
It’s a simple technique, but it’s useful.
Another good practice is to keep production references from repeat orders. If the customer returns six months later and orders the same antique bronze finish, the factory has something physical to compare against.
Buyers can help enormously by maintaining their own retained samples too.
Don’t depend entirely on emailed photographs from the previous order.
Physical references reduce arguments, shorten re-sampling time, and give both parties a much more objective basis for approving repeat production.
Quality Inspection for Antique Charger Plates
Inspection should evaluate both the molded product and its decorative finish.
A charger plate can have a perfect color but still fail because it’s warped. It can also have excellent dimensions but fail because the antiquing is inconsistent.
That’s why a sensible inspection plan covers several categories.
As the molded body, inspect dimensions, shape, rim integrity, stability, obvious molding defects, and physical damage.
For the finish, examine color, antiquing balance, gloss, surface cleanliness, scratches, coating loss, and consistency against approved references.
Coming to packaging, verify protective separation, carton quantity, labels, inner packaging, carton condition, and any custom barcode or private-label requirements.
A useful B2B inspection framework looks like this:
| Inspection Area | Typical Check | Buyer Benefit |
|---|---|---|
| O'lchamlar | Diameter and key dimensions | Prevents mismatch with table settings |
| Tekislik | Stable placement on flat surface | Reduces rocking or warped pieces |
| Molded detail | Rim pattern and edge | Protects design quality |
| Yakunlash | Compare with approved sample | Controls visual consistency |
| Yuzaki | Scratches, dirt, exposed substrate | Reduces complaints |
| Coating | Agreed adhesion check if specified | Helps identify weak finishing |
| Handling resistance | Agreed rub/abrasion method | Predicts decorative durability |
| Paketlash | Separation and carton protection | Reduces transit scratching |
| Labeling | SKU, barcode, carton marks | Simplifies distribution |
One common sourcing mistake is approving a beautiful sample but leaving the purchase specification vague.
Later, the buyer says, “This isn’t the same antique gold.”
The supplier replies, “Antique finishes naturally vary.”
Both statements may be partly true.
The solution is to define the allowable range before mass production.
For substantial wholesale programs, pre-shipment inspection can include random sampling from multiple cartons and different areas of the production batch.
If the product will be supplied repeatedly, inspection records and retained samples become even more valuable.
They transform quality management from memory and opinion into a repeatable process.
OEM and Custom Antique Finish Charger Plates
OEM production becomes much easier when buyers separate customization into four decisions:
shape, pattern, finish, and packaging.
You may not need a new mold at all.
If an existing plate shape already suits your market, changing the decorative treatment can create a different collection at substantially lower development complexity than opening completely new tooling.
Typical customization possibilities can include antique gold, vintage silver, bronze, copper-inspired finishes, distressed black-and-gold effects, alternative rim patterns, private labeling, custom cartons, barcode labels, and assortment packaging.
For a new project, a professional RFQ should provide:
- Required diameter and shape
- Reference image or physical sample
- Preferred antique color
- Expected order quantity
- Destination market
- Intended application
- Qadoqlash talablari
- Logo or private-label requirement
- Target launch date
- Any required compliance or testing documentation
The last point is especially important.
Don’t simply ask, “Do you have certificates?”
Tell the manufacturer what country you’re importing into, what claims you plan to make, how the plate will be used, and which documentation your customer or retailer requires.
That allows the factory to determine what actually applies.
For custom finishes, sampling normally deserves more attention than buyers first expect.
A metallic gold displayed on your laptop can look substantially different on a molded plate under warm restaurant lighting. Likewise, heavy antiquing that looks dramatic in a close-up photograph may make an entire banquet table appear much darker.
Ask for samples and evaluate them in the environment where the product will be sold or used.
For distributors, it can also be useful to test the plate with common tablecloth colors, dinnerware, glassware, cutlery, and centerpiece styles.
You’re not purchasing a plate in isolation.
You’re purchasing part of a visual table-setting system.
Common Manufacturing Problems and How Buyers Can Avoid Them
Most quality problems aren’t mysterious. They usually come from poorly defined expectations, unstable processing, inadequate handling, or insufficient inspection.
Uneven antiquing is one of the most common concerns.
Some variation is intentional, but extreme light and dark differences can make a batch look inconsistent. Approving boundary samples before production helps establish the acceptable range.
Poor coating adhesion is more serious.
If decorative layers detach during normal handling, the issue may involve surface preparation, coating compatibility, processing conditions, curing, or another part of the finish system. The factory should investigate the process rather than simply touching up affected pieces.
Scratches during packing can occur even when the finish itself is good.
Metallic surfaces tend to reveal scratches clearly. Protective bags, tissue, dividers, foam, or other separation methods can therefore be part of product engineering, not just logistics.
Color mismatch between repeat orders is another risk.
The phrase “same as last time” isn’t a reliable technical specification unless one or both parties retained an approved physical reference.
The strongest sourcing habit is simple:
turn visual preferences into documented approval standards.
That means keeping the approved sample, identifying the finish code, recording packaging details, and making important inspection requirements part of the purchase agreement.
Buyers should also avoid judging color from one photo sent through a messaging app. Camera white balance, workshop lighting, reflections, phone displays, and image compression can all change the apparent finish.
For critical projects, use photographs for communication and physical samples for approval.
It’s a small distinction, but in decorative manufacturing, it can prevent large disagreements.
How Should You Specify Antique Charger Plates to a Manufacturer?
The best quotation begins with a good specification.
If your inquiry only says, “Please quote antique gold charger plate,” the supplier still has several unanswered questions.
What diameter?
Which rim?
How dark should the aging effect be?
How many pieces?
What packaging?
Do you need an existing design or custom tooling?
What market will the goods enter?
A good RFQ removes those uncertainties early.
For example, rather than requesting “antique gold,” provide a reference photo and explain that you want a warm gold base with dark brown shading concentrated around recessed decorative areas, moderate gloss, and no heavy black appearance on the center.
That’s much easier for a sample team to interpret.
Your approval workflow can then follow a simple structure:
reference → factory sample → buyer comments → revised sample if necessary → signed master sample → pilot or mass production → inline inspection → final inspection
For new designs or high-volume programs, don’t rush the sample merely to save a few days.
Sampling is inexpensive compared with correcting thousands of finished pieces.
Buyers should also distinguish between must-have characteristics and preferences.
Plate diameter may be mandatory.
Color family may be mandatory.
The exact location of every tiny antique mark probably shouldn’t be.
Remember, a distressed aesthetic depends on variation. Trying to specify every irregular mark would defeat the purpose and make production unnecessarily complicated.
The goal is to establish the product’s identity and acceptable range.
Once that’s documented, the manufacturer can concentrate on process control and your inspection team has a meaningful standard to work against.
That is how an artistic-looking finish becomes a scalable B2B product.
FAQs About Antique Finish Charger Plates
Are antique finishes created by using real aged metal?
Usually not for molded decorative plastic charger plates. The aged-metal appearance is commonly created through decorative finishing techniques over a molded substrate. Buyers should confirm the exact material and coating construction with their supplier for each product.
Why does the antique finish vary slightly between plates?
Part of the effect comes from controlled differences in shading, highlights, recesses, and surface texture. Small variation can make the finish look natural. Large variations, however, should be controlled with master samples and inspection standards.
Can antique charger plates be customized in different colors?
Yes. Depending on the factory’s finishing capability, antique-style collections may be developed in gold, silver, bronze, copper-inspired, champagne, pewter, or mixed dark-and-metallic effects. Physical sample approval is recommended before bulk manufacturing.
Can a manufacturer match an existing antique charger plate sample?
Often, a factory can develop a close visual reference if you provide a physical sample. Exact replication isn’t always practical because substrates, coating systems, textures, and processing methods differ. Agree on an acceptable comparison standard before production.
How should buyers test the durability of the decorative coating?
Start by defining the expected application and handling conditions. Buyer and manufacturer can then agree on visual, adhesion, rub, or abrasion evaluations. Recognized standards may help establish methods, but their applicability should be confirmed for the specific coating system.
Are decorative charger plates safe for direct food contact?
Don’t assume so. A charger plate is commonly used beneath dinnerware as a decorative presentation piece. Direct food-contact suitability should only be claimed when the specific material, coating system, intended use, and applicable compliance documentation support that claim.
How can buyers prevent color differences between repeat orders?
Keep an approved physical master sample and ask the manufacturer to retain one as well. Record the factory finish code, specifications, and packaging requirements so future production can be compared against the same reference.
Should buyers approve charger plate colors from photos?
Photos are useful for initial communication, but they shouldn’t be the only approval method for color-sensitive orders. Lighting, cameras, reflections, and screens can alter metallic colors considerably. A physical sample is much more reliable.
Conclusion: Turning an Antique Look Into a Repeatable Product
The most attractive antique charger plates combine artistic appearance with disciplined manufacturing control.
The aged effect itself comes from layers: a properly molded substrate, suitable surface preparation, a metallic foundation, controlled darkening or distressing, and an appropriate protective finish.
But for a B2B buyer, the real value comes from what happens around those layers.
A manufacturer needs to reproduce the appearance across production quantities, manage reasonable variation, protect the finish during packing, and inspect the goods against agreed references.
That’s why successful sourcing shouldn’t begin with only the question:
“How much is your antique gold charger plate?”
A better conversation includes the application, quantity, size, finish reference, durability expectations, packaging, destination market, and approval process.
When these details are defined early, sampling becomes faster and production risk falls.
For wholesale, retail, hospitality, wedding supply, event rental, and private-label programs, we recommend using a physical master sample plus a written product specification as the final production reference.
That gives the buyer and manufacturer the same target.
If you’re developing an antique gold, antique silver, bronze, copper-inspired, or custom distressed charger plate collection, send your reference photo or physical sample, required diameter, estimated quantity, destination market, and packaging requirements to the manufacturing team.
We can then evaluate the suitable existing mold or OEM route, prepare finish samples, define the approval standard, and quote the project based on your actual requirements rather than a generic product description.
For repeat wholesale programs, request a retained master sample and documented finish specification before mass production. This small step can make future reorders significantly easier and more consistent.